Non-contact precision cutting
Wire EDM Services
Precision wire electrical discharge machining for intricate profiles, hardened metals, sharp internal features, and tight-tolerance components.
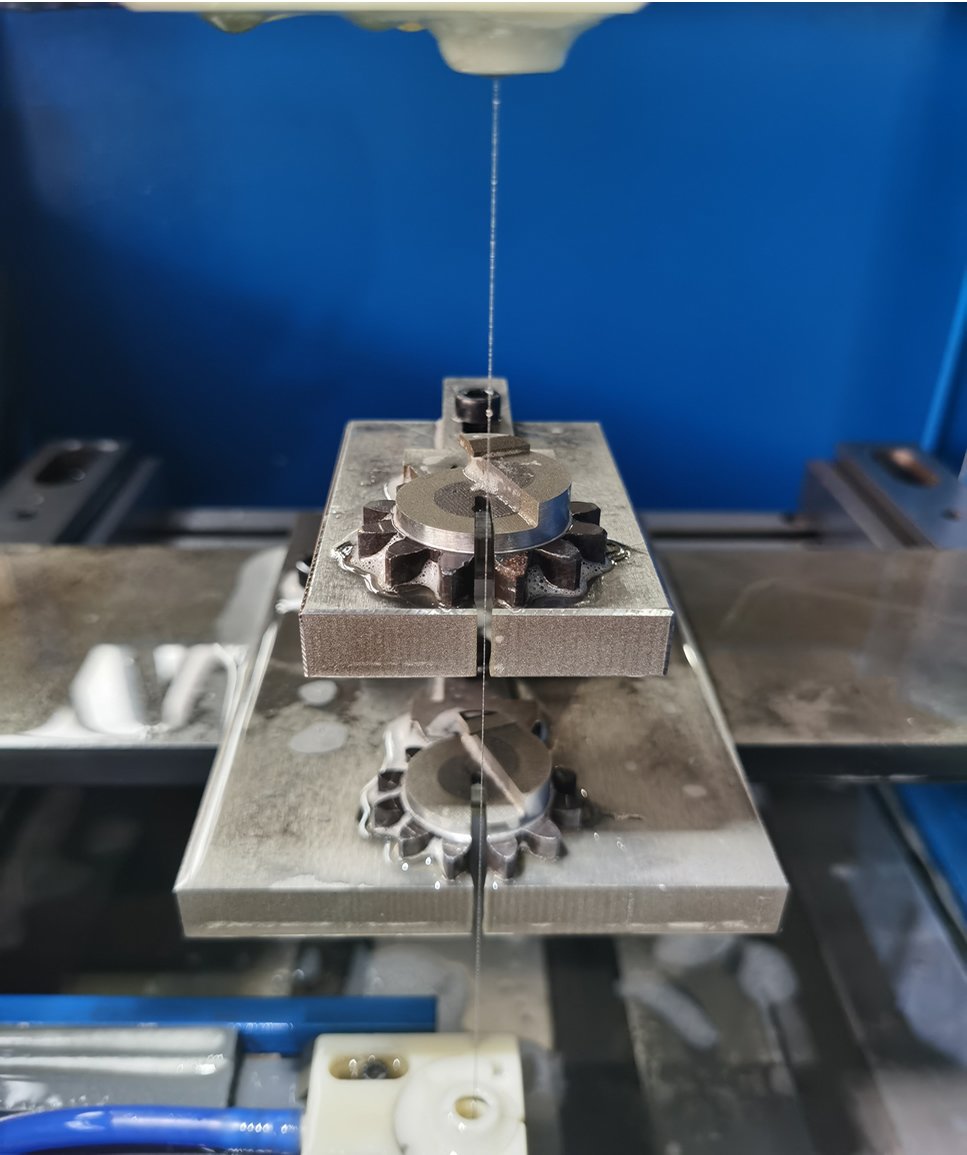
6CNC provides wire cut EDM services for tooling, inserts, precision mechanical parts, prototypes, and small batches. The non-contact process removes conductive material with a controlled electrical discharge, avoiding conventional cutting forces on delicate or hardened components.
Conductive metals and alloys
Straight, tapered and intricate profiles
Hardened material capability
Prototype and small-batch support
Precision Wire EDM Capabilities
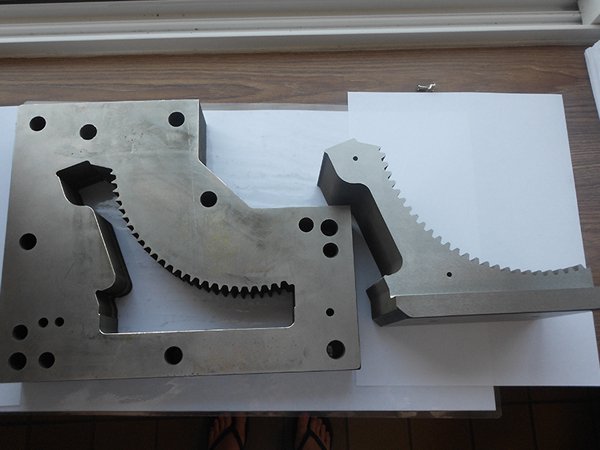
Intricate 2D Profiles
Cut complex external and internal contours, slots, windows, forms, and precision openings from conductive materials.
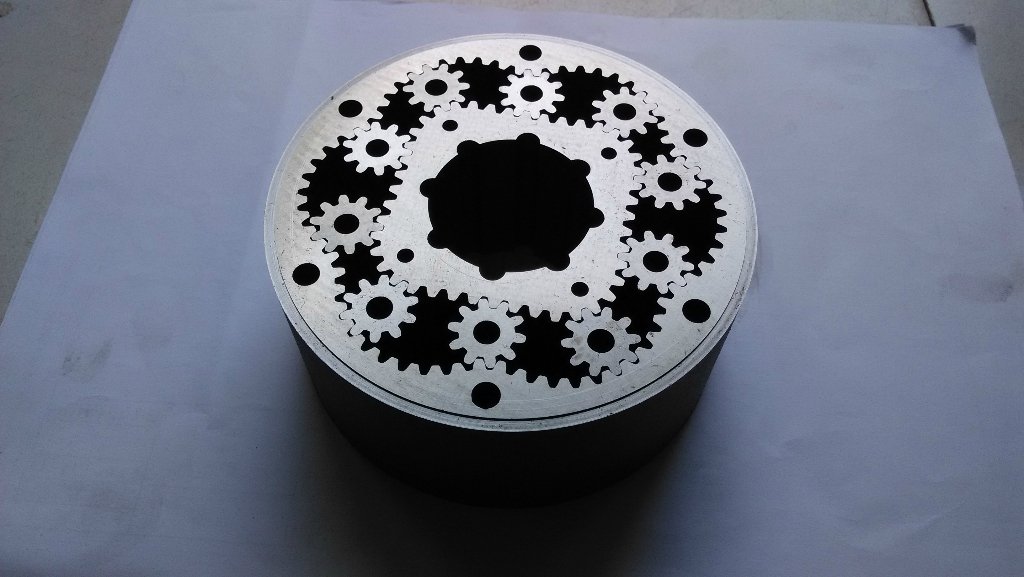
Hardened Components
Machine selected heat-treated steels, carbide, and hard alloys without relying on conventional cutting hardness.
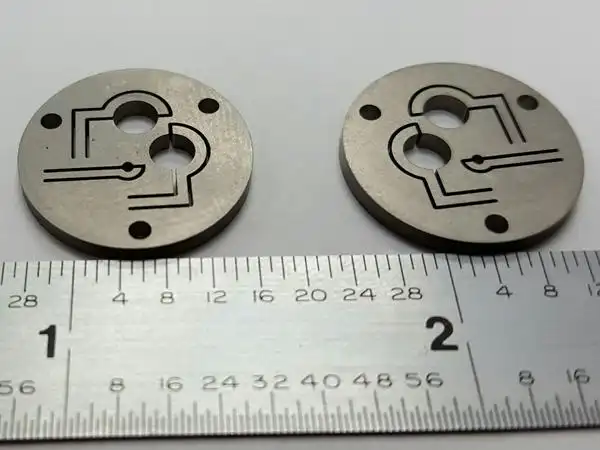
Taper Cutting
Review straight or tapered walls for dies, inserts, electrodes, guides, and precision mechanical components.
Small Internal Radii
Produce fine details and controlled radii subject to wire diameter, spark gap, workpiece thickness, and access.
Stack and Batch Cutting
Selected flat components may be stacked or nested when geometry, accuracy, flushing, and traceability permit.
Combined CNC + EDM
Coordinate milling, turning, grinding, drilling, heat treatment, and wire EDM through one project route.
Precision Profiles Without Conventional Cutting Pressure
Wire EDM is valuable when the component is hard, delicate, narrow, or difficult to machine with a rotating cutter. Because the wire does not mechanically contact the workpiece, thin sections and intricate profiles can often be produced with lower risk of cutting-force deflection.
The process is limited to electrically conductive materials. A programmed wire path passes through the workpiece while controlled discharges remove material in dielectric fluid. Rough cutting establishes the profile; additional skim passes may improve dimensional accuracy and surface condition.
6CNC engineers review material, thickness, profile complexity, corner radii, taper, start holes, clamping, datums, tolerances, surface finish, and inspection needs before quotation.
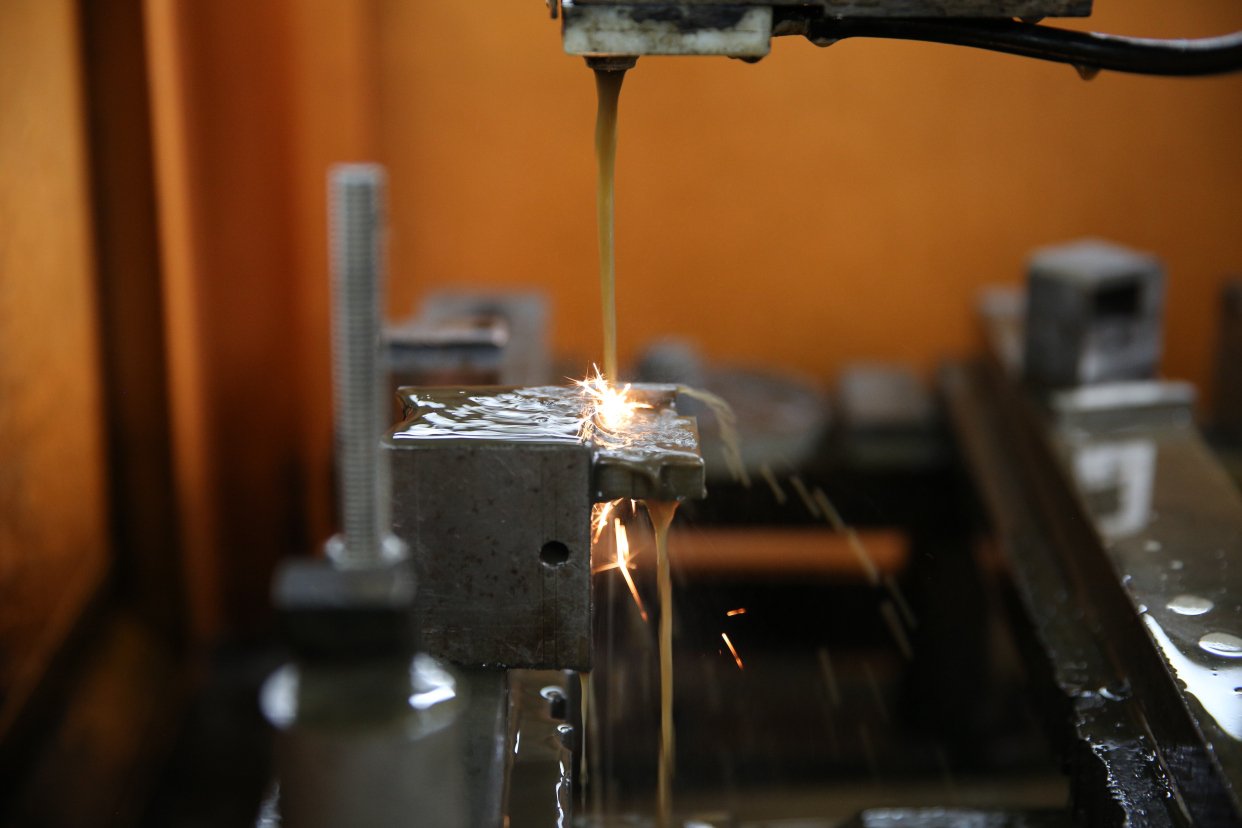
6CNC Wire Cut EDM Process
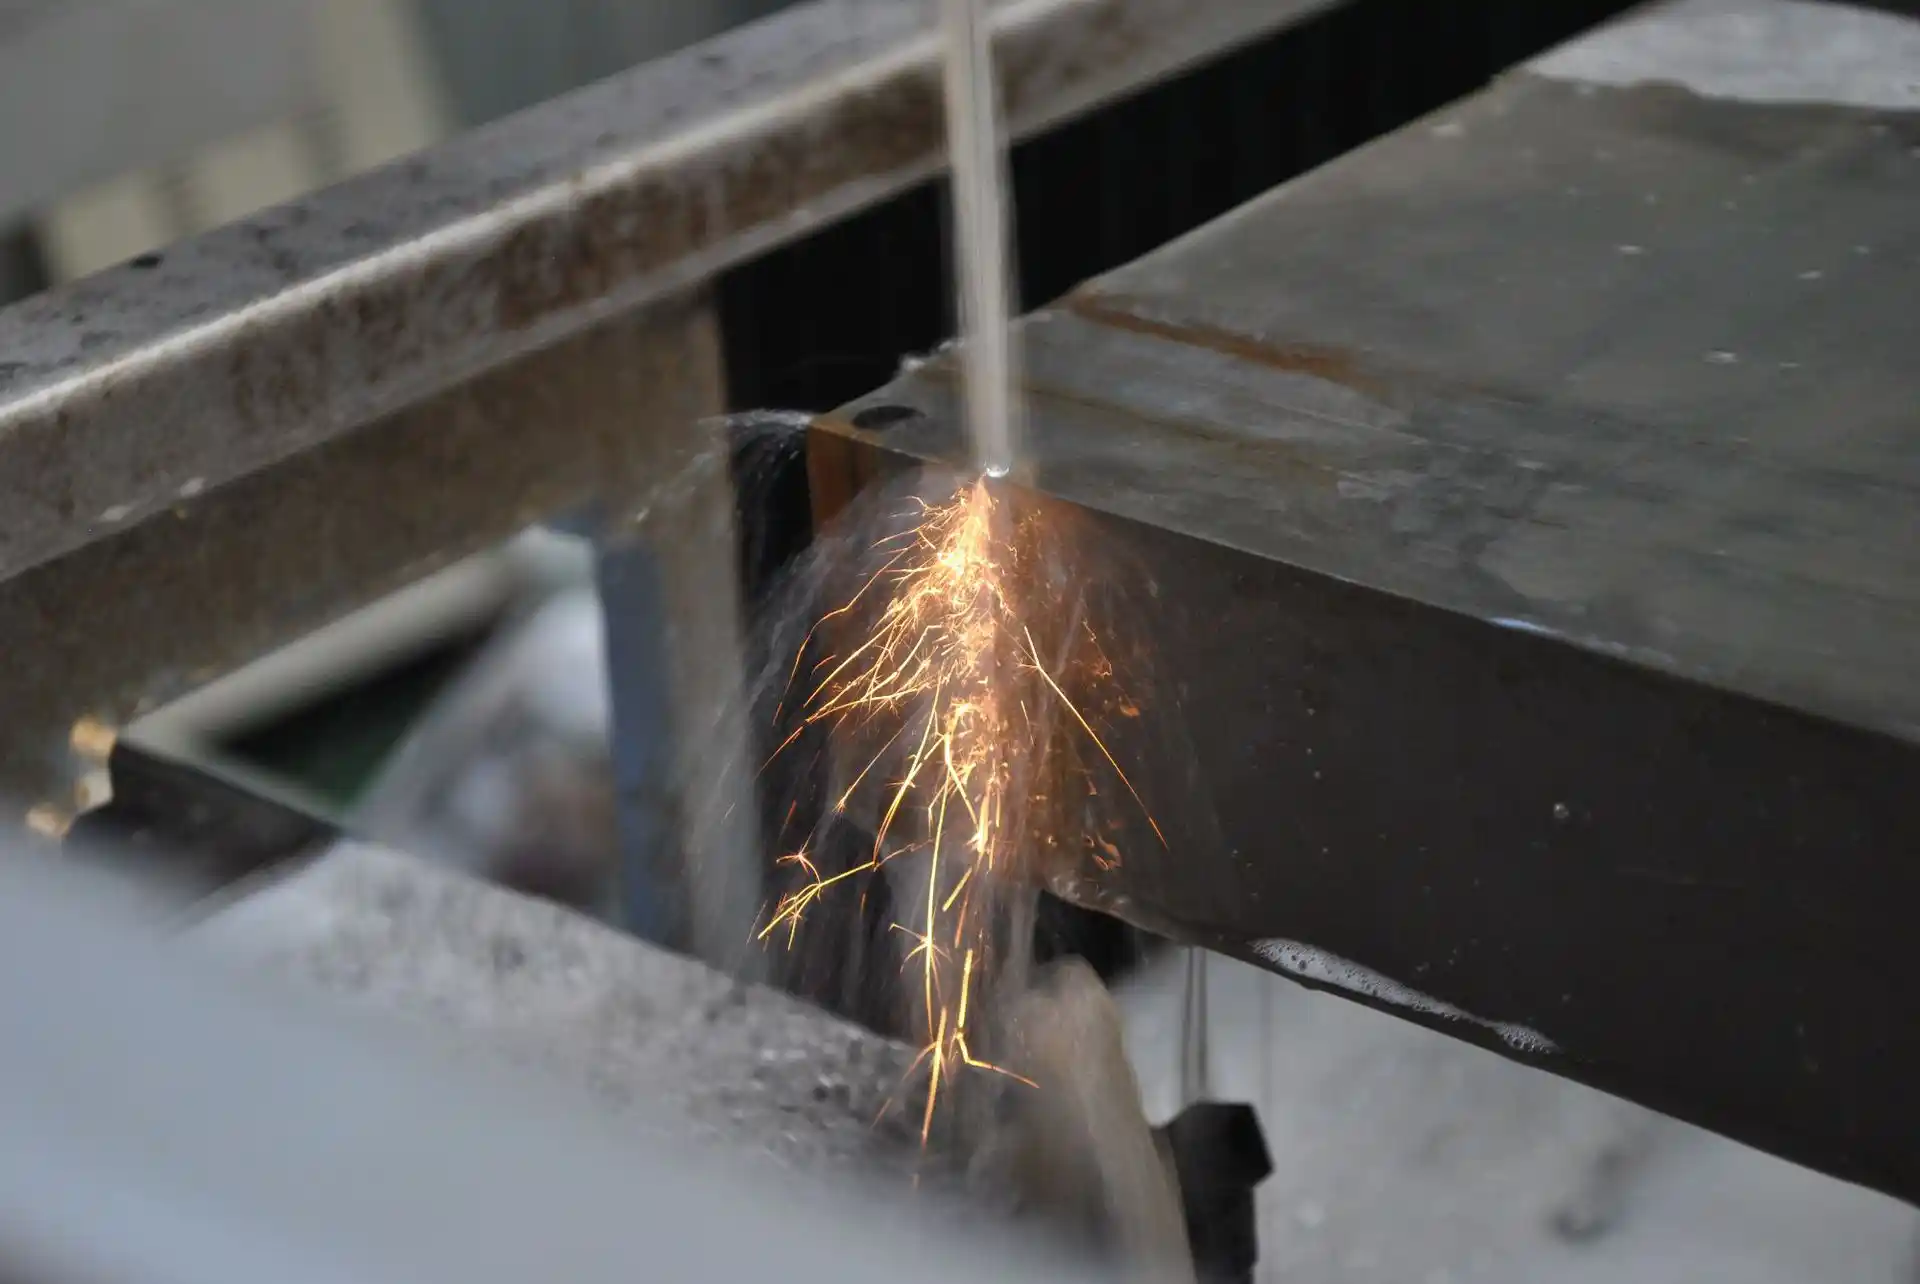
Drawing Review
Confirm material, thickness, datums, tolerances, corner radii, taper, surface finish, quantity, and inspection requirements.
Workpiece Preparation
Machine blanks and reference features, complete heat treatment where appropriate, and establish clamping surfaces.
Start-Hole Planning
Create or confirm start holes for closed contours while protecting critical finished surfaces.
Rough Wire Cut
Remove the majority of material using a stable programmed path and controlled discharge conditions.
Skim Passes
Apply additional trim cuts where needed to improve accuracy, geometry, and surface condition.
Inspection
Verify profiles, positions, thickness relationships, and drawing-defined features before delivery.
Materials for Wire Electrical Discharge Machining
Material group
Tool and mold steels
Examples
D2, H13, A2 and drawing-specified grades
Typical applications
Dies, punches, inserts, forms, tooling
Carbon and alloy steels
Examples
1045, 4140, 4340 and hardened grades
Typical applications
Precision machine parts, wear components
Stainless steels
Examples
303, 304, 316, 17-4 PH
Typical applications
Medical, laboratory, food, and industrial parts
Carbide
Examples
Selected cemented carbide grades
Typical applications
Wear parts, punches, tooling inserts
Aluminum and copper alloys
Examples
Aluminum, copper, brass, bronze
Typical applications
Electrodes, instruments, precision components
Titanium and nickel alloys
Examples
Drawing-specified conductive alloys
Typical applications
Aerospace, energy, and demanding equipment
Nonconductive plastics, ceramics, and composites cannot be cut by standard wire EDM unless they have a suitable conductive condition or specialized process route.
Tight-Tolerance EDM and Quality Control
Profile Accuracy
Contour dimensions and locations are verified relative to the drawing datums.
Corner Radii
Minimum radii are reviewed against wire diameter, spark gap, material, thickness, and finish strategy.
Taper and Straightness
Wall angle, verticality, and profile consistency are evaluated over the cut height.
Surface Condition
Rough and skim-cut strategies are selected around functional finish requirements.
Thermal and Stress Control
Material condition, prior heat treatment, residual stress, and part support are considered in process planning.
Inspection Documentation
Dimensional reports, material documents, and project-specific records are available when agreed.
Common Wire EDM Applications
Dies and Punches
Precision cutting edges, die openings, punches, stripper plates, and inserts.
Mold Components
Slides, lifters, inserts, shutoffs, and difficult internal profiles.
Aerospace Parts
Hardened or difficult-alloy profiles, slots, test components, and tooling.
Medical Components
Small conductive parts, instrument components, fixtures, and development hardware.
Precision Machinery
Guides, gauges, wear plates, keys, slots, and alignment components.
Electronics
Connector tooling, lead-frame tooling, small conductive profiles, and fixtures.
Automotive Tooling
Stamping, forming, checking fixtures, prototypes, and maintenance components.
Repair and Legacy Parts
Low-volume replacement components made from drawings or engineering data.
Common questions
FAQ About Wire EDM Services
What is wire EDM?
Wire electrical discharge machining uses a continuously moving conductive wire and controlled electrical sparks to cut electrically conductive material without direct tool contact.
What materials can wire EDM cut?
Wire EDM can cut conductive materials including tool steel, stainless steel, alloy steel, aluminum, copper, brass, carbide, titanium, and nickel alloys, subject to drawing review.
Can wire EDM cut hardened steel?
Yes. Material hardness has less influence on the removal mechanism than in conventional cutting, making wire EDM suitable for many pre-hardened and heat-treated components.
Does wire EDM create cutting forces?
The process is non-contact, so it does not impose conventional milling or turning forces. Thermal effects and residual stress still require process planning.
Can wire EDM produce sharp internal corners?
It can produce small internal radii, but a perfectly sharp internal corner is not possible because the wire has a physical diameter and requires spark clearance.
Can you cut tapers with wire EDM?
Selected taper angles and variable profiles can be reviewed according to part thickness, geometry, machine travel, accuracy, and wire guidance.
What tolerances can wire EDM hold?
Achievable tolerance depends on material, thickness, profile, feature length, machine setup, thermal control, number of skim passes, and inspection method. Specify the required tolerance on the drawing.
What surface finish is available?
Surface finish depends on cut strategy and the number of trim or skim passes. State critical finish requirements on the drawing for quotation.
Is a start hole required?
Closed internal contours normally require a start hole unless the design allows threading from an open edge or another process route is agreed.
Do you support prototype and small-batch wire EDM?
Yes. We support one-off components, prototypes, tooling, repair parts, and repeat small batches.
Start your project
Get a Precision Wire EDM Quote
Upload your CAD model and controlled drawing with material, thickness, tolerances, surface-finish requirement, start-hole information, quantity, and inspection notes.